


Products Description
API 5L X80 seamless pipe is a high-strength low-alloy line pipe grade specified under API Specification 5L / ISO 3183, with a minimum yield strength of 555 MPa (80,500 psi) . It is the highest mainstream grade in the standard API 5L ladder, positioned above X70 and below the still-emerging ultra-high-strength grades X90/X100/X120. In the ISO designation system, X80 corresponds to L555; the European equivalent is EN 10208-2 L555MB, and the Canadian equivalent is CSA Z245.1 Grade 555.
X80 is a specialist grade, not a drop-in replacement for X70. Its economic justification lies in wall-thickness reduction: for the same operating pressure, an X80 line can use thinner wall than X65 or X70, cutting steel tonnage, welding time, and coating consumption on large-diameter, long-distance, high-pressure gas transmission projects. Seamless X80 is particularly relevant for thick-wall, high-pressure service where the pipe body must carry the design load without a seam weld, and for station piping, headers, and fittings where a seamless product simplifies fabrication and inspection.
| Parameter | Typical Export Range | Notes |
| Outside diameter (OD) | 21.3 mm – 610 mm (NPS ½ – 24″) | Seamless X80 is commonly quoted up to 24″; larger OD is normally LSAW territory |
| Nominal pipe size (NPS) | ½″ – 24″ | 12″, 16″, 18″, 20″, and 24″ are standard export inquiries |
| Wall thickness | SCH 10 – SCH 160, plus STD, XS, XXS | SCH 40 – SCH 160 covers most high-pressure seamless X80 demand |
| Length | 5.8 m / 6 m / 11.8 m / 12 m; SRL (5–7 m) / DRL (10–12 m) | Fixed or random length per project |
| End finish | Beveled, plain end, threaded & coupled, grooved | Plastic caps standard on beveled ends |
| Surface / coating | Bare, varnished, black painting; 3PE / 3PP / 2PE / 2PP, FBE, cement mortar lining | Coating selected to project specification |
Typical export size table (representative, not exhaustive):
| NPS | OD (mm) | Common Schedules | Typical WT Range (mm) | Typical Seamless Availability |
| 6″ | 168.3 | SCH 40 – SCH 160 | 7.1 – 18.3 | Yes |
| 8″ | 219.1 | SCH 40 – SCH 160 | 8.2 – 23.0 | Yes |
| 10″ | 273.1 | SCH 40 – SCH 160 | 9.3 – 28.6 | Yes |
| 12″ | 323.9 | SCH 40 – SCH 160 | 10.3 – 33.3 | Yes |
| 16″ | 406.4 | SCH 40 – SCH 120 | 12.7 – 30.2 | Yes |
| 20″ | 508 | SCH 40 – SCH 120 | 15.1 – 35.0 | Mill-dependent |
| 24″ | 610 | SCH 40 – SCH 100 | 17.5 – 30.0 | Mill-dependent; confirmP |
packaging & Shipping
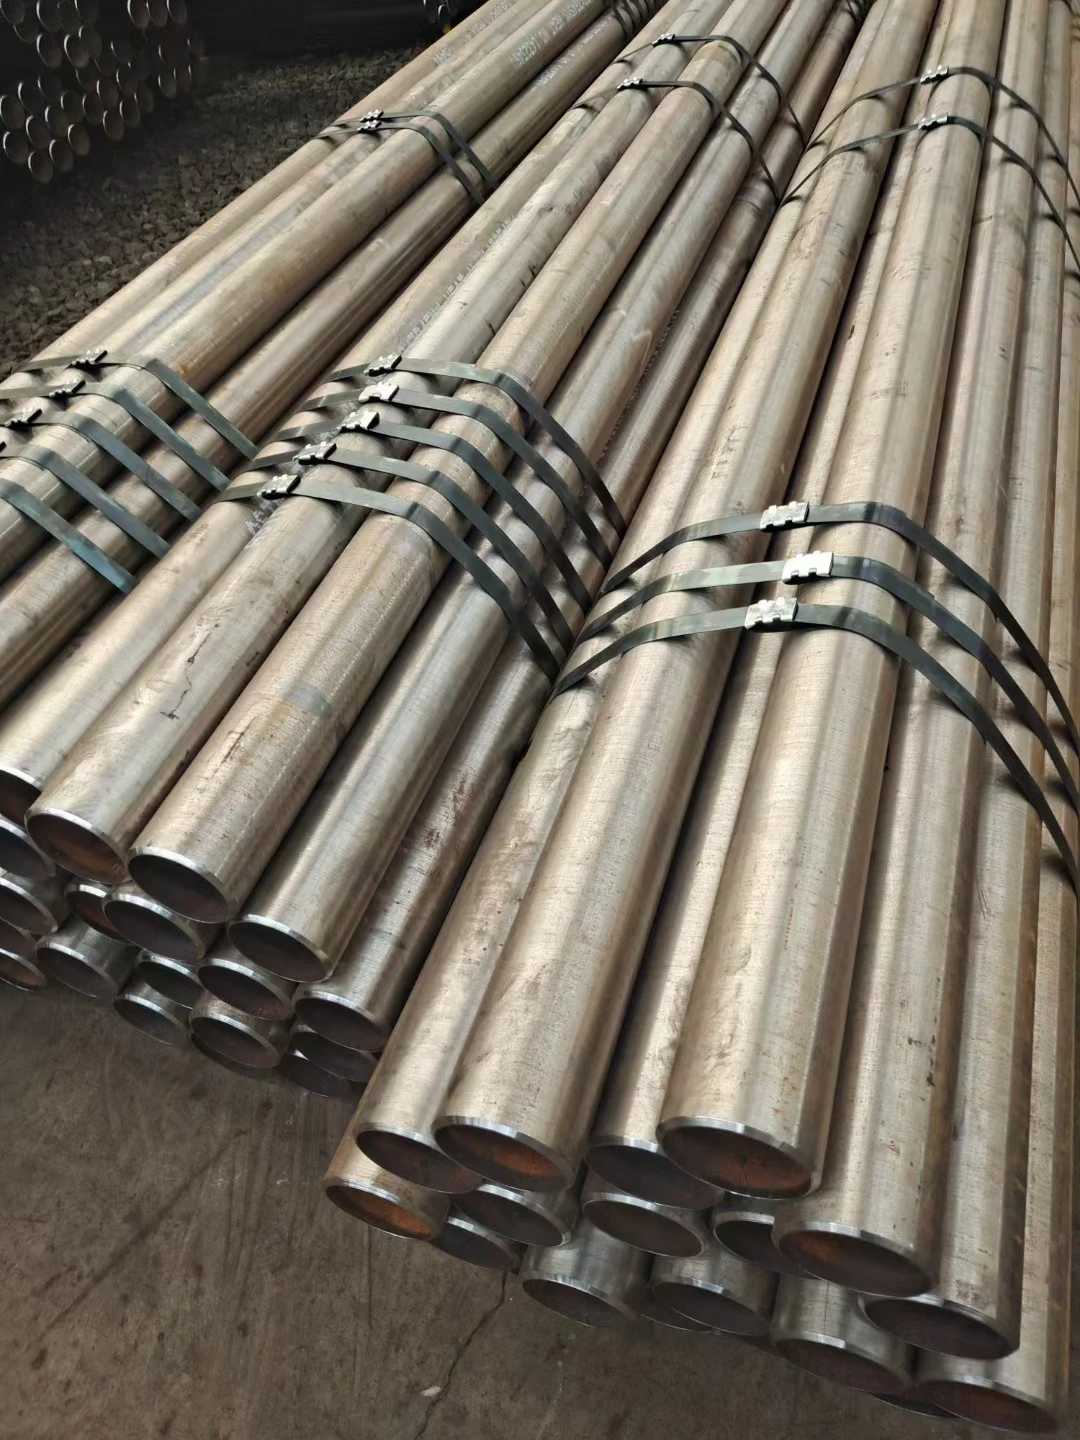
- Packing: Bundled with steel strips, plastic end caps for pipe ends; large diameter loose loading
- Surface: Bare black, varnish, or anti-corrosion coating as required
- Shipping port: Tianjin, Qingdao, Shanghai
- Shipping term: FOB, CFR, CIF, DAP, DDP
- MOQ: Small trial order acceptable; bulk order for full container (20GP / 40GP / 40HQ)
- Lead time: Stock sizes 7–15 days; customized production 25–45 days

Technical Specifications
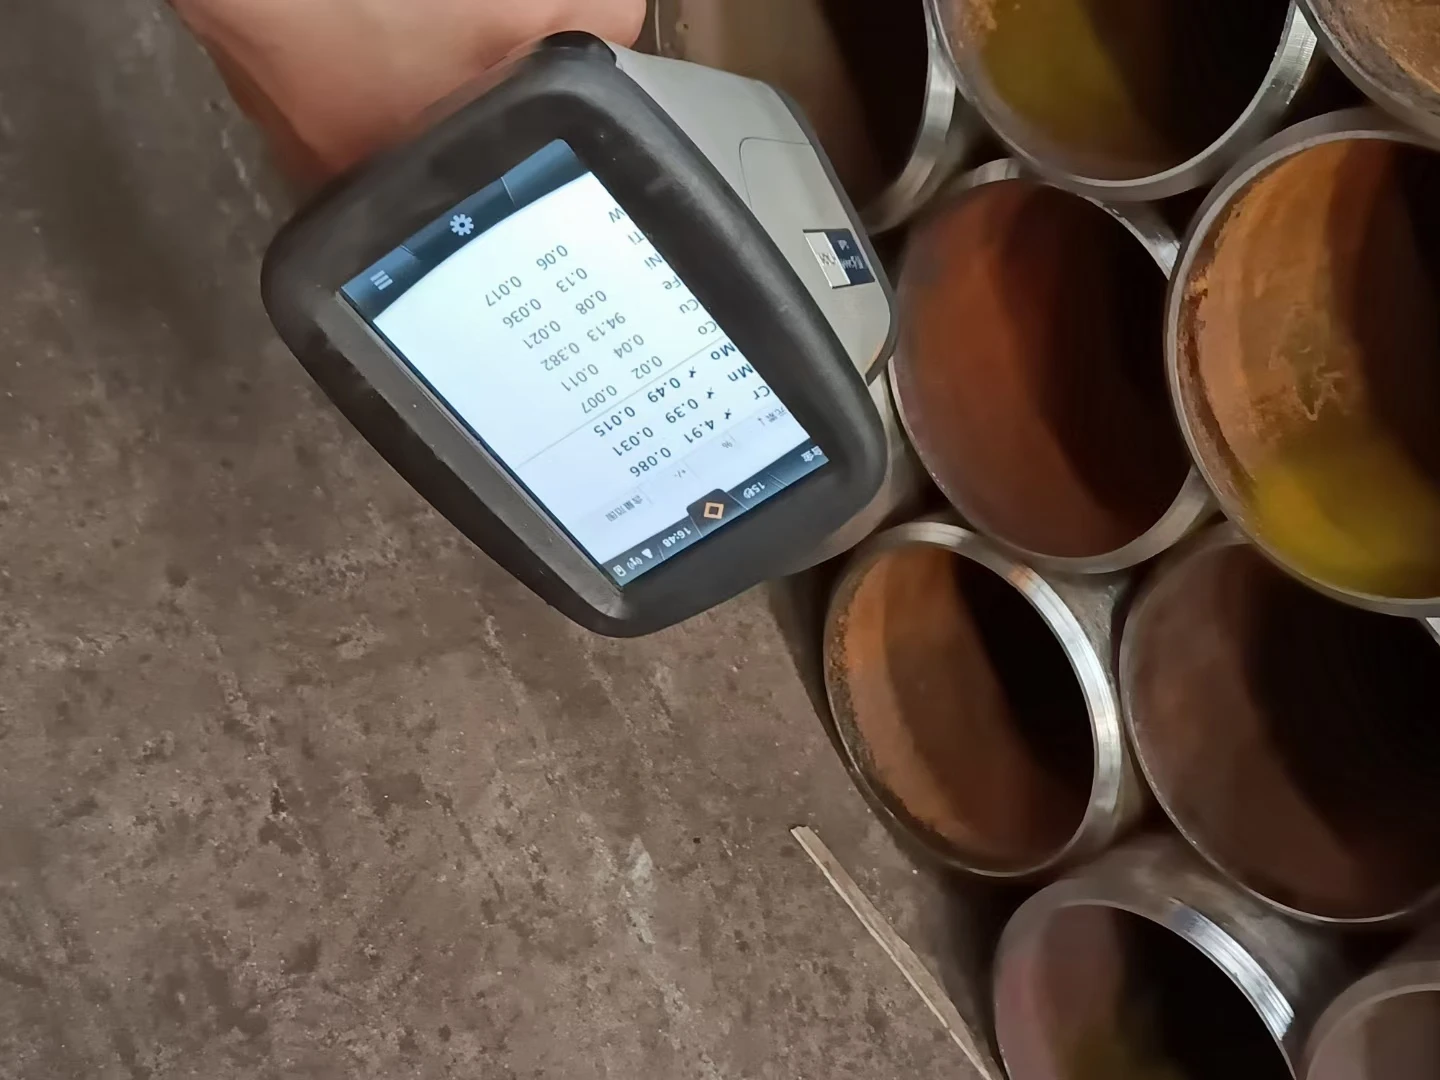
1.Chemical Composition (PSL2, X80M / X80Q Seamless):
For X80Q seamless with wall thickness > 20 mm, CE_IIW limits are subject to mandatory agreement per API 5L Table 5; CE limits must always be confirmed with the mill at order placement. Published project-level limits also appear as CE_IIW ≤ 0.43 and Pcm ≤ 0.25; the governing value is the one agreed on the purchase order and verified against the MTC.
| Element / Parameter | X80M Seamless (max, %) | X80Q Seamless (max, %) | Technical Function |
| Carbon (C) | 0.1 | 0.18 | Weldability and HAZ hardness control |
| Manganese (Mn) | 1.85 | 1.85 | Primary strength / transformation-control element |
| Silicon (Si) | 0.45 | 0.45 | Deoxidation |
| Phosphorus (P) | 0.02 | 0.02 | Residual / toughness control |
| Sulfur (S) | 0.01 | 0.01 | Residual / toughness control |
| Nb + V + Ti (total) | 0.15 | 0.15 | Grain refinement + precipitation hardening |
| Mo (where used) | 0.50 max | 0.50 max | Hardenability / thick-wall strength |
| Ni (where used) | 1.00 max | 1.00 max | Toughness / thick-wall hardenability |
| CE_IIW (max) | By agreement - typically ≤ 0.46 | By agreement - typically ≤ 0.46 | Weldability / HAZ cracking risk |
| Pcm (max) | By agreement - typically ≤ 0.22 | By agreement - typically ≤ 0.25 | Low-carbon crack parameter |
2.Mechanical Properties (PSL2 Pipe Body):
| Property | X80M / X80Q PSL2 | Equivalent (ksi) | Notes |
| Minimum yield strength (SMYS) | 555 MPa | 80.5 ksi | Grade identity |
| Maximum yield strength | 705 MPa | 102.3 ksi | PSL2 ceiling - controls over-strength |
| Minimum tensile strength (SMTS) | 625 MPa | 90.6 ksi | Confirms pipe body strength after processing |
| Maximum tensile strength | 825 MPa | 119.7 ksi | Prevents excessive strength with reduced ductility |
| Yield-to-tensile ratio (max) | 0.93 | - | Mandatory PSL2 limit for deformation behavior |
| Elongation (min) | Per API 5L formula | - | Calculated on applicable test piece |
The strength window is a defining feature of X80 PSL2: both minimum and maximum limits apply to yield and tensile strength. This ceiling protects ductility and ensures that pipe sections deform in a controlled manner before a girth weld is overloaded in a tension event.
3.Impact Toughness (CVN, PSL2):
| Test Location | Temperature | Minimum Average Absorbed Energy | Reference |
| Pipe body - longitudinal | 0 °C | ≥ 101 J | X80-specific PSL2 requirement |
| Pipe body - transverse | 0 °C | ≥ 68 J | X80-specific PSL2 requirement |
| Weld / HAZ | −10 °C | ≥ 27 J | Common project specification |
PSL2 requires CVN impact testing for the pipe body, and for welded pipe also the weld seam and HAZ; X80 carries a higher body-toughness floor than lower grades, reflecting its service in high-pressure gas transmission. Drop-weight tear testing (DWTT) is specified where fracture-arrest control is a design requirement.
4.Delivery Conditions: X80M vs X80Q:
| Condition | Designation | Process | Typical Wall Thickness | Typical Product Form | Primary Use |
| TMCP | X80M / L555M | Thermomechanical controlled rolling, no post-roll full heat treatment | Up to ~25 mm | LSAW large-diameter pipe; seamless where applicable | Mainline gas transmission, large OD |
| Q&T | X80Q / L555Q | Quenched and tempered after rolling | 15 mm and above | Seamless or heavy-wall LSAW | High-pressure thick-wall, station piping, headers |
For seamless X80, the X80Q (Q&T) route is the relevant delivery condition for thick-wall, high-pressure applications; X80M is predominantly an LSAW mainline product. Other delivery conditions listed in the broader API 5L framework - as-rolled, normalized, normalized and tempered - are generally not used to achieve the X80 strength-toughness balance; TMCP and Q&T are the practical routes.
Applications
- Long-distance natural gas main transmission pipelines
- Crude oil & condensate oil trunk pipelines
- Oil & gas gathering pipeline networks
- Underground storage pipeline, injection pipeline
- River crossing, mountain crossing, cold region pipeline projects
- Industrial high-pressure process piping (non-sour / sour service upon test)
- Export to Central Asia, Middle East, South America, Southeast Asia, Africa pipeline projects
FAQ
Q1: Is API 5L X80 available in PSL1?
No. X80 is produced exclusively as PSL2. API 5L does not define PSL1 chemistry or mechanical requirements for grades above X70. Every X80 order automatically carries PSL2 mandatory CVN impact testing, NDT, tighter chemistry control, and heat/test-unit traceability.
Q2: Can X80 be used for sour service (NACE MR0175 / ISO 15156)?
Standard API 5L X80 is not a sour-service grade, and there is no mainline Annex H/I X80 variant. NACE MR0175 hardness and SSC resistance limits generally drive sour-service material selection toward lower-strength grades or specially qualified X70QS/X70MS. X80 may be considered only after project-specific HIC/SSC qualification and explicit mill agreement - it cannot be assumed interchangeable with a sour-service specification.
Q3: What is the difference between X80M and X80Q?
The suffix indicates the delivery heat-treatment route. X80M is thermomechanically controlled rolled (TMCP) with no post-roll full heat treatment; it is the default for large-diameter LSAW mainline pipe and is available in wall thicknesses up to approximately 25 mm. X80Q is quenched and tempered after rolling; it is the relevant condition for seamless X80, especially in thick-wall, high-pressure service at 15 mm and above. X80Q seamless with WT > 20 mm requires mandatory CE agreement with the mill.
Q4: What CVN impact values does X80 PSL2 require?
For X80 PSL2 pipe body, the full-size 0 °C average absorbed energy is ≥ 101 J longitudinal and ≥ 68 J transverse. This is a grade-specific X80 requirement under PSL2; PSL1 has no impact requirement at all. Weld and HAZ toughness limits are typically set by project specification (a common reference is ≥ 27 J at −10 °C).
Q5: What is the maximum seamless X80 size available?
Seamless X80 is commonly available up to 24″ OD (610 mm) , with wall thickness from SCH 40 through SCH 160 depending on mill and delivery condition. Above 24″, X80 is normally supplied as LSAW or SSAW. For NPS 20″–24″, seamless availability is mill-dependent and should be confirmed with a specific enquiry including OD, WT, length, and delivery condition.
Q6: Can I weld X80 with the same procedure as X70?
No. X80 requires full WPS re-qualification under API 1104 or ASME IX. Key changes include a stricter diffusible-hydrogen limit (≤ 4 ml/100 g), a narrower heat-input window (1.0–3.0 kJ/mm), a lower maximum interpass temperature (230 °C), and mandatory CVN testing on weld metal and HAZ. Reusing an X70 WPS with minor amendments is a recognized failure mode on X80 projects.
Q7: What testing and documentation accompany an X80 PSL2 order?
A complete X80 PSL2 technical record includes: heat and test-unit traceability linked to the MTC; chemical analysis including CE_IIW and/or Pcm; tensile tests confirming yield and tensile strength within the 555–705 MPa / 625–825 MPa window; CVN impact tests on pipe body (and weld/HAZ for welded pipe); NDT (UT or PAUT) for PSL2; hydrostatic testing; and dimensional inspection. Third-party inspection (SGS, BV, TÜV, etc.) is available on request.
Q8: What is the difference between X80 and X70 in wall thickness and cost?
X80's higher SMYS allows approximately 10–12% wall-thickness reduction versus X70 PSL2 and 17–18% versus X65 at the same design pressure. However, X80 carries a material-cost premium, narrower mill availability, and higher welding-qualification cost. The upgrade pays back on large-diameter, long-distance, high-pressure projects where tonnage and weld volume dominate total installed cost; on shorter or lower-pressure projects, X70 remains the more economic choice.
Our address
Rm1406,14th/F No 208, Hongqi Road, Nankai Dist, Tianjin City ,China
Phone Number(whatsApp/Wechat)
+8616622033809
alisa@tjshenzhoutong.com

Hot Tags: api 5l x80 line pipe seamless steel tube, China api 5l x80 line pipe seamless steel tube manufacturers, suppliers, factory, seamless pipe for air conditioning systems, seamless pipe for efficiency system connection, seamless pipe for heat exchangers, seamless pipe for inspection system connection, seamless pipe for mechanical system connection, seamless pipe for redundancy system connection


